


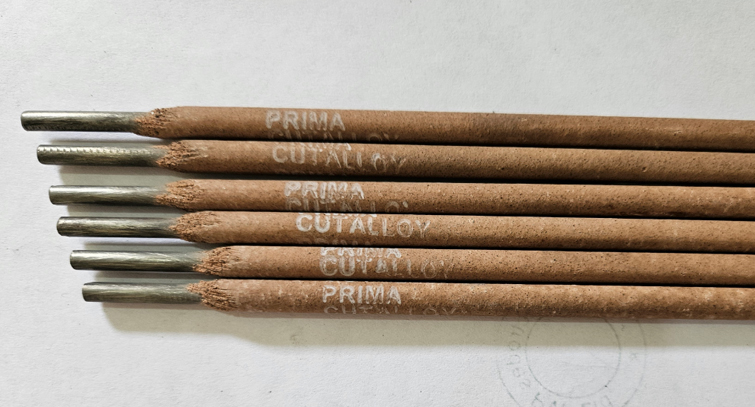
IDENTIFICATION: NAME PRINTED |
CURRENT CONDITION AC or DC (+) |
Characteristics:
A medium coated electrode specially designed for faster and smoother cutting, piercing and beveling of all kinds of ferrous and non ferrous metals, medium and high alloy steels and cast iron.
Typical Applications
It can be used with ease for cutting and piercing out of position jobs where gas cutting is not convenient.
Welding Current (Amps) |
||
5.0 mm |
4.00 mm |
3.15 mm |
240 – 300 |
200 – 300 |
200 – 150 |
Welding Technique
Hold the electrode pointing towards job to be cut at an angle of 45 Degree and use sawing motion to cut. The forceful arc produced by the electrode and sawing motion ensure fast cutting. Similarly for piercing hold the electrode perpendicular to the job and use push in and pull out action till the job is pierced. Dry electrode before use at 160-2000C for one hour.
Dimensions & Weight Specification of Electrodes |
|||
Dia, mm |
5.0 |
4.0 |
3.15 |
Length mm |
350/450 |
350/450 |
350/450 |
Wt. per Carton Kg. |
3.5 |
3.5 |
3.5 |
Wt. per Box, Kg. |
14 |
14 |
14 |
IDENTIFICATION: NAME PRINTED |
CURRENT CONDITION AC or DC (+) |
Characteristics:
Designed to Produce smooth grooves in all positions. Withstand high, current without heating. The forceful arc renders it possible to chamfer and gouge various metals without the need of supplementary gas, air oxygen or special torches. The force of the arc blows away undesired materials from its path leaving a clean groove.
Typical Applications
Mark the area to be gouged or chamfered with chalk. Hold the electrode pointing towards the path at an angel not exceeding 25 Degree to the job. Push the electrode along the line maintaining contact with the base metal.
Welding Current (Amps) |
||
5.0 mm |
4.00 mm |
3.15mm |
250 – 330 |
300 – 400 |
190 – 290 |
Dimensions & Weight Specification of Electrodes |
|||
Dia,mm |
5 |
4 |
3.15 |
Length mm |
350/450 |
350/450 |
350/450 |
Wt.per Carton Kg. |
2 |
2 |
2 |
Wt.per Box, Kg. |
12 |
12 |
12 |
