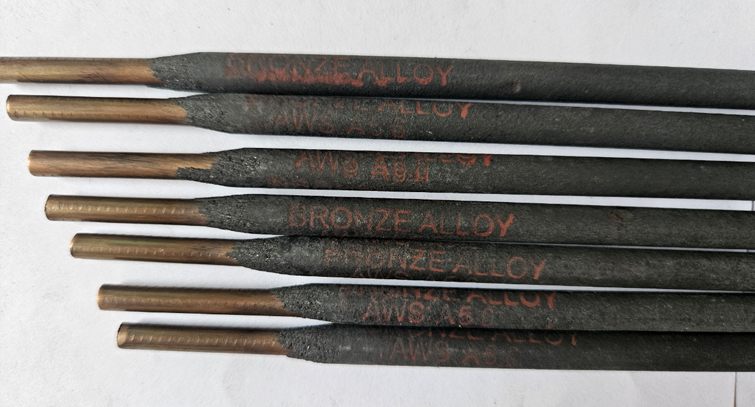
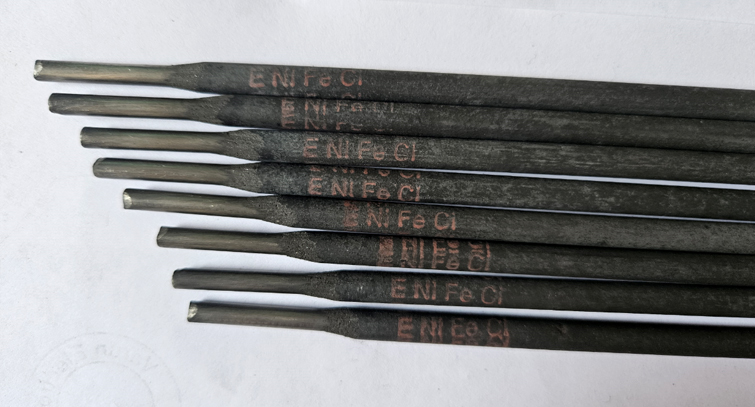
CLASSIFICATION |
AWS A 5.11 |
E Ni Cr Mo 3 |
IDENTIFICATION: NAME PRINTED |
CURRENT CONDITION AC OR DC (±) |
Characteristics:
Basic coated electrode with Ni-Cr-Fe type nickel base deposit. Used for repairing and joining of nickel alloys, 5 - 9% Nickel steels, cryogenic stainless steels down to -196°C, Incoloy 800 and other high temperature steels. For joining dissimilar materials as stainless steels/low alloyed steels, stainless steels/Nickel alloys, buffering of difficult to weld steels. Weld metal deposit is insensitive to cracks, has very good resistance to acids, salts and alkaline solutions, molten salt (e.g. cyanide) in oxidizing and arburization atmospheres (avoid a sulphurous atmosphere).
Typical Applications:
Chemical industries, petrochemical industries, glassworks, civil engineering, repairing and maintenance workshops. Generally used for welding on oven parts, burners, heat treatment equipment, cement works, moulds, transport and storage tanks of liquid gas.
Welding Current (Amps) |
|||
5.00mm |
4.00mm |
3.15mm |
2.50 |
150 - 180 |
110 - 140 |
80 - 100 |
70 - 90 |
Weld Metal Chemistry: (%)
All Weld Mechanical Properties: |
|||
UTS |
550 N/mm2 Min |
Elong. (5d) |
30% Min. |
Dimensions & Weight Specification of Electrodes |
||||
Dia mm |
5.00 |
4.00 |
3.15 |
2.50 |
Length mm |
350 |
350 |
350 |
350 |
Wt. per Carton Kgs |
2 |
2 |
2 |
2 |
Wt. per Box |
12 |
12 |
12 |
12 |
CLASSIFICATION |
AWS : A5.11 |
E Ni Cu 7 |
IDENTIFICATION: NAME PRINTED |
CURRENT CONDITION AC or DC (+) |
Characteristics:
A basic type electrode depositing 65 Ni 30 Cu weld metal, having soft and smooth arc, with almost no spatter producing X ray qulity weld metal. The weld metal posses excellent mechanical properties
Typical Applications
The electrode is suited for welding Ni Cu alloys, monel to monel, mixed assembly of alloys without chromium and on surfacing of parts used in sea water desalination plants, waste water treatment plant electroplating and chemical pickling equipment.
Welding Current (Amps) |
||
5.0 mm |
4.00 mm |
3.15 mm |
160-180 |
120-150 |
90-100 |
Weld Metal Chemistry: (%) |
|||
C |
0.15 Max |
Fe |
2.50 Max |
Mn |
4.00 Max |
Ni |
62.0 – 69.0 |
Si |
1.50 Max |
Cu |
Remainder |
P |
0.02 Max |
S |
0.015 max |
All Weld Mechanical Properties: |
||||
UTS |
500 N/mm2 Min |
Elong. (5d) |
30% Min |
|
Dimensions & Weight Specification of Electrodes |
|||
Dia, mm |
5.00 |
4.00 |
3.15 |
Length mm |
350 |
350 |
350 |
Wt. per Carton Kg. |
2.0 |
2.0 |
2.0 |
Wt. per Box, Kg. |
12 |
12 |
12 |
CLASSIFICATION |
AWS:A 5.6 |
ECuSn-A |
IDENTIFICATION: NAME PRINTED |
CURRENT CONDITION AC or DC (+) |
Characteristics:
A phosphor-Bronze electrode which is characterized by good welding performance such as steady arc, low spatter, easy de-slagging and defect free, shining weld deposit. The electrode can be operated easily on both AC as well as DC (+) in all conventional positions.
Typical Applications
Suitable for joining copper to copper alloys, phosphor and tin bronzes as well as copper plates and for surfacing on copper and copper alloys. Typical applications of the electrode include marine components, pump castings, impellers, gear teeth and copper & Bronze Bushings. The electrode is also suitable for overlaying applications.
Welding Current (Amps) |
|
4.0 mm |
3.15 mm |
110-160 |
60-110 |
Weld Metal Chemistry: (%) |
|||
Sn |
4.0-6.0 |
Cu |
90-92 |
P |
0.35 Max |
Fe |
2.0 Max |
All Weld Mechanical Properties: |
||||
Uts |
300-340 N/mm2 |
Weld Metal |
75-85 BHN |
|
Elong . 5d |
30-35 % |
Hardness |
|
|
Dimensions & Weight Specification of Electrodes |
||
Dia, mm |
4.00 |
3.15 |
Length mm |
350 |
350 |
Wt.per Carton Kg. |
2.0 |
2.0 |
Wt.per Box, Kg. |
12 |
12 |