


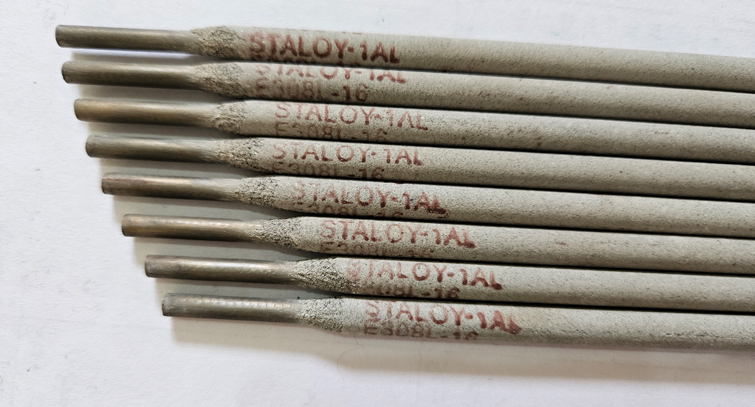
IDENTIFICATION: NAME PRINTED |
CURRENT CONDITION |
Characteristics:
A low carbon 19 Cr. 10 Ni stainless electrode with controlled ferrite. The weld metal is highly resistant to cracking corrosion and oxidation at high temp. upto 8000C. The weld metal has excellent creep strength and is of radiographic quality.
Typical Applications:
The electrode can be used for welding AISI 301, 302, 304 & 308 and equivalent stainless steel grades.
Welding Current (Amps) |
||||
5.0mm |
4.0mm |
3.15mm |
2.5mm |
|
150-180 |
110-140 |
80-100 |
50-80 |
|
Weld Metal Chemistry: (%) |
|||
| C | 0.10 Max | S | 0.03 Max |
Mn |
2.00 Max |
Cr. |
18.0-21.0 |
Si |
0.90 Max |
Ni |
8.0-11.0 |
P |
0.03 Max |
|
|
All Weld Mechanical Properties: |
|||
UTD |
560 N/mm2 Min |
Ferrite % |
5 - 7 |
Elong. (5d) |
30% Min |
|
|
Dimensions & Weight Specification of Electrodes |
|||||
Dia, mm |
5.0 |
4.0 |
3.15 |
2.50 |
2.00 |
Length mm |
350 |
350 |
350 |
350 |
350 |
Wt. per Carton Kg. |
2.0 |
2.0 |
2.0 |
2.0 |
2.0 |
Wt. per Box, Kg. |
10 |
10 |
10 |
10 |
10 |
CLASSIFICATION |
AWS/ A5.4 |
IS : 5206-83 |
IDENTIFICATION: NAME PRINTED |
CURRENT CONDITION |
Approved and Certified by:
Research Designs & Standards Organisation Class M2.
Characteristics:
A semi basic type stainless steel electrode giving extra low carbon 19 Cr. 10 Ni controlled ferrite weld metal which is highly resistant to cracking and corrosion. Weld metal is of radiographic quality and offers excellent corrosion, resistance to various media. Scaling and oxidation resistance is satisfactory upto 8000C.
Typical Application
The electrode can be used for welding AISI 301, 302, 304, 304L, 308 & 308 L and equivalent stainless steel grades.
Welding Current (Amps) |
||||
5.0mm |
4.0mm |
3.15mm |
2.5mm |
2.00 mm |
150-180 |
110-140 |
80-100 |
50-80 |
35-50 |
Weld Metal Chemistry: (%) |
|||
C |
0.04 Max |
Mn |
2.00 Max |
Si |
0.90 Max |
P |
0.03 Max |
S |
0.03 Max |
Cr. |
18.0-21.0 |
Ni |
8.0-11.0 |
|
|
All Weld Mechanical Properties: |
|
Utd |
560 N/mm2 Min |
Elong. (5d) |
30% Min |
Dimensions & Weight Specification of Electrodes |
|||||
Dia, mm |
5.0 |
4.0 |
3.15 |
2.50 |
2.00 |
Length mm |
350 |
350 |
350 |
350 |
350 |
Wt. per Carton Kg. |
2.0 |
2.0 |
2.0 |
2.0 |
2.0 |
Wt. per Box, Kg. |
10 |
10 |
10 |
10 |
10 |
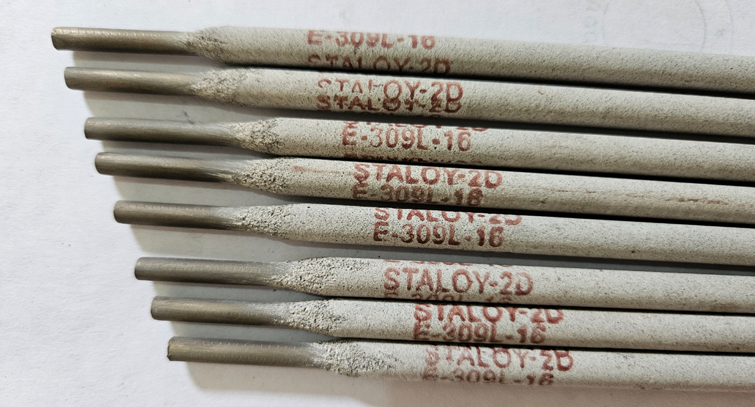
IDENTIFICATION: NAME PRINTED |
CURRENT CONDITION |
Characteristics:
A rutile coated electrode depositing high Cr & Ni having excellent resistance to corrosion and oxidation upto 11000C. The electrode gives excellent radiographic quality weld besides similar stainless steels.
Typical Applications :
It is extensively used in dissimilar metal joining between MS and Low alloy steel and stainless steel, overlaying and buffering applications, welding straight chromium steel etc.
Welding Current (Amps) |
||
5.0mm |
4.0mm |
3.15mm |
150-180 |
85-140 |
80-60 |
All Weld Mechanical Properties: |
|||
UTS |
540 – 635 N/mm2 |
Elong. (5d) |
42% Min |
Dimensions & Weight Specification of Electrodes |
|||
Dia, mm |
5.0 |
4.0 |
3.15 |
Length mm |
350 |
350 |
350 |
Wt. per Carton Kg. |
2.0 |
2.0 |
2.0 |
Wt. per Box, Kg. |
10 |
10 |
10 |
CLASSIFICATION |
AWS/ A5.4 E 347L-16 |
IS : 5206-83 E-19.9 L Nb R26 |
IDENTIFICATION: NAME PRINTED |
CURRENT CONDITION AC(>70 V) or DC (+) |
Characteristics:
A semi basic low carbon 19/10 Cb stainless steel electrode with controlled ferrite content 4-9% for maximum resistance to cracking corrosion at high temperature. Cb prevents carbide precipitation at high temp. so high creep strength.
Typical Applications:
Radiographic quality weld and may be used for the welding on AISI Steel 321, 347 and 18-8 steel.
Welding Current (Amps) |
|||
5.0 mm |
4.00 mm |
3.15 mm |
|
150-180 |
110-140 |
80-100 |
|
Weld Metal Chemistry: (%) |
|||
C |
0.03 Max |
Mn |
1.0-2.0 |
Si |
0.90 Max |
P |
0.03 Max |
S |
0.03 max |
Cr |
18.0-21.0 |
Ni |
9.0-11.0 |
Cb |
0.5 Min |
All Weld Mechanical Properties: |
|||
UTS |
590 N/mm2 Min |
Impact at |
70 Joules Min |
Elong. (5d) Ferrite % |
38% Min 5-7 |
27°C |
|
Dimensions & Weight Specification of Electrodes |
||||
Dia, mm |
5.0 |
4.0 |
3.15 |
2.50 |
Length mm |
350 |
350 |
350 |
350 |
Wt. per Carton Kg. |
2.0 |
2.0 |
2.0 |
2.0 |
Wt. per Box, Kg. |
10 |
10 |
10 |
10 |
CLASSIFICATION |
AWS/ A5.4 |
E 410 Ni Mo - 15 |
IDENTIFICATION: NAME PRINTED |
CURRENT CONDITION |
Characteristics:
Staloy 4A(L) is a Basic Electrode Cr-Ni, 12/5 for weld 13 Cr/1 Ni to 13 Cr/6 Ni, ASTM CA6NM, AISI 410 Steels and Protective Coatings of wearing by cavitation and erosion by water in turbine rotor fans. Deposit Hardness with the air-cooling ~450 HB. Oxidation resistant up to 800ºC.
Typical Applications:
Weld of Special Steels used in Equipments of Hydroelectric Mills, as Turbine Wheels, Francis and Pelton and its components, resistant to corrosion by cavitations of sweet or Salted Water up to 450ºC, Valve Seats.
Welding Current (Amps) |
|||
5.0 mm |
4.00 mm |
3.15 mm |
2.50 mm |
130-160 |
100-130 |
80-100 |
50-80 |
Weld Metal Chemistry: (%) (All single values are maximum) |
|||
C |
0.04 |
S |
0.012 |
Mn |
0.60 - 0.90 |
Cr. |
11.50 - 14.00 |
Si |
0.50 Max |
Ni |
4.00 - 6.00 |
P |
0.016 |
Mo |
0.40 - 0.60 |
All Weld Mechanical Properties: (All single values are minimum): |
|||
UTS |
760 N/mm2 |
Elong. (5d) |
16% |
Dimensions & Weight Specification of Electrodes |
||||
Dia, mm |
5.00 |
4.0 |
3.15 |
2.50 |
Length mm |
350 |
350 |
350 |
350 |
Wt. per Box Kgs |
2.0 |
2.0 |
2.0 |
2.0 |
Wt. per Carton Kgs |
10 |
10 |
10 |
10 |
CLASSIFICATION |
AWS/ A5.4 |
IS : 5206-83 |
E 316L-15 |
E-19.12 LR 26 |
IDENTIFICATION: NAME PRINTED |
CURRENT CONDITION |
Characteristics:
A rutile coated electrode depositing extra low carbon 18 Cr-12 Ni-2.3 Mo weld metal. The deposit exhibits exceptional corrosion resistance to acids and salts and has very good resistance to pitting attack by chlorides. Intergranular corrosion resistance is excellent. The weld metal being particularly immune to sensitization during welding.
Typical Applications:
Ideally suited for welding stainless steel of similar composition. Weld metal has very good creep strength.
Welding Current (Amps) |
|||
5.0 mm |
4.00 mm |
3.15 mm |
2.5 mm |
150-180 |
110-140 |
80-100 |
50-80 |
Weld Metal Chemistry: (%) |
|||
C |
0.04 Max |
S |
0.03 Max |
Mn |
2.00 Max |
Cr. |
17.0-20.0 |
Si |
0.90 Max |
Ni |
11.0-14.0 |
P |
0.03 Max |
Mo |
2.0-3.0 |
All Weld Mechanical Properties: |
|||
UTS |
500 N/mm2 Min |
Ferrite % |
3 - 8 |
Elong. (5d) |
30% Min |
|
|
Dimensions & Weight Specification of Electrodes |
||||
Dia, mm |
5.0 |
4.0 |
3.15 |
2.50 |
Length mm |
350 |
350 |
350 |
350 |
Wt. per Carton Kg. |
2.0 |
2.0 |
2.0 |
2.0 |
Wt. per Box, Kg. |
10 |
10 |
10 |
10 |
CLASSIFICATION |
AWS/ A5.4 |
E 307 - 16 |
IDENTIFICATION: NAME PRINTED |
CURRENT CONDITION |
Characteristics:
Rutile based high strength, fully austenitic electrode, designed to resist heat and impact. Fully machinable weld deposit will work harden under impact and retain properties at high temperatures specially developed for steels difficult to weld, such as armor plates and austenitic high Mn-steels.
Typical Applications:
Armor plate, Hardenable steels including steels difficult to weld, Non-magnetic austenitic steels Work hardening austenitic manganese steels, Dissimilar joints, Problem steels.
Welding Current (Amps) |
|||
5.0 mm |
4.00 mm |
3.15 mm |
2.5 mm |
150-180 |
110-140 |
80-100 |
50-80 |
Weld Metal Chemistry: (%) |
|||
C |
0.13 Max |
S |
0.02 Max |
Mn |
4.80 – 7.00 |
Cr. |
18.50 - 21.50 |
Si |
0.50 Max |
Ni |
8.50 - 11.00 |
P |
0.04 Max |
Mo |
1.00 Max |
All Weld Mechanical Properties: |
|||
YS |
300 N/mm2 Min |
Elong. (5d) |
25% Min |
UTS |
540 N/mm2 Min |
Impact at 20°C |
70 J Min |
Dimensions & Weight Specification of Electrodes |
||||
Dia, mm |
5.0 |
4.0 |
3.15 |
2.50 |
Length mm |
350 |
350 |
350 |
350 |
Wt. per Carton Kg. |
2.0 |
2.0 |
2.0 |
2.0 |
Wt. per Box, Kg. |
10 |
10 |
10 |
10 |
CLASSIFICATION |
AWS/ A5.4 |
E 410 Ni Mo - 15 |
IDENTIFICATION: NAME PRINTED |
CURRENT CONDITION |
Characteristics:
Staloy 4A(L) is a Basic Electrode Cr-Ni, 12/5 for weld 13 Cr/1 Ni to 13 Cr/6 Ni, ASTM CA6NM, AISI 410 Steels and Protective Coatings of wearing by cavitation and erosion by water in turbine rotor fans. Deposit Hardness with the air-cooling ~450 HB. Oxidation resistant up to 800ºC.
Typical Applications:
Weld of Special Steels used in Equipments of Hydroelectric Mills, as Turbine Wheels, Francis and Pelton and its components, resistant to corrosion by cavitations of sweet or Salted Water up to 450ºC, Valve Seats.
Welding Current (Amps) |
|||
5.0 mm |
4.00 mm |
3.15 mm |
2.5 mm |
150-180 |
110-140 |
80-100 |
50-80 |
Weld Metal Chemistry: (%) |
|||
C |
0.04 Max |
S |
0.012 Max |
Mn |
0.60 – 0.90 |
Cr. |
11.50 - 14.00 |
Si |
0.50 Max |
Ni |
4.00 - 6.00 |
P |
0.016 Max |
Mo |
0.40 – 0.06 |
All Weld Mechanical Properties: |
|||
YS |
550 N/mm2 Min |
Elong. (5d) |
16% Min |
UTS |
760 N/mm2 Min |
Impact at 20°C |
70 J Min |
Dimensions & Weight Specification of Electrodes |
||||
Dia, mm |
5.0 |
4.0 |
3.15 |
2.50 |
Length mm |
350 |
350 |
350 |
350 |
Wt. per Carton Kg. |
2.0 |
2.0 |
2.0 |
2.0 |
Wt. per Box, Kg. |
10 |
10 |
10 |
10 |
CLASSIFICATION |
AWS/ A5.4 E |
IS : 5206-83 E18.8MnR26 |
IDENTIFICATION: NAME PRINTED |
CURRENT CONDITION DC (+) |
Characteristics:
A basic heavy coated multipurpose stainless steel electrode, easy to operate in all position at low current. The weld metal has excellent crack resistance as well as heat resistances! 900°C. It is also corrosion resistant to atmosphere, marine water and weak acids. It gives 18% Cr, 8% Ni and 5% Mn type weld deposit, Slag easily Removable.
Typical Applications:
Suitable for joining ferritic to austenitic steels, armor plates, heat resistant steels, and dissimilar materials. Buffers layers on difficult steels before hard facing. Excellent for repairing cracks in austenitic manganese steel, castings for surfacing manganese steel.
Welding Current (Amps) |
||
5.0 mm |
4.00 mm |
3.15 mm |
180-220 |
130-170 |
90-120 |
Weld Metal Chemistry: (%) |
|||
C |
0.20 Max |
Mn |
5.00 – 8.00 |
Si |
0.90 Max |
P |
0.04 Max |
S |
0.03 max |
Cr |
17.0-20.00 |
Ni |
7.00 – 11.00 |
Mo. |
0.50 Max |
All Weld Mechanical Properties: |
|||
UTS |
510 N/mm2 Min |
Elong. (5d) |
20% Min |
Dimensions & Weight Specification of Electrodes |
||||
Dia, mm |
5.00 |
4.00 |
3.15 |
2.50 |
Length mm |
350 |
350 |
350 |
350 |
Wt. per Carton Kg. |
2.0 |
2.0 |
2.0 |
2.0 |
Wt. per Box, Kg. |
10 |
10 |
10 |
10 |
CLASSIFICATION |
AWS/ A5.4 E 312 |
IS : 5206-83 |
IDENTIFICATION: NAME PRINTED |
CURRENT CONDITION |
Characteristics:
A rutile basic electrode specially designed for welding similar and dissimilar steels. Electrode produces crack free high strength joints in carbon steel, low alloy steel stainless steel including difficult to weld steels.
Typical Applications:
Ideally suited for welding of a variety of unknown compositions steel, leaf and coil spring & other difficult to weld steels.
Welding Current (Amps) |
|||
5.0 mm |
4.00 mm |
3.15 mm |
2.5 mm |
150-180 |
110-140 |
80-100 |
60-80 |
Weld Metal Chemistry: (%) |
|||
C |
0.15 Max |
S |
0.03 Max |
Mn |
2.00 Max |
Cr. |
26.0 -30.0 |
Si |
0.90 Max |
Ni |
8.0-12.0 |
P |
0.03 Max |
|
|
All Weld Mechanical Properties: |
|
UTS |
580 N/mm2 Min |
Elong. (5d) |
30% Min |
Dimensions & Weight Specification of Electrodes |
||||
Dia, mm |
5.0 |
4.0 |
3.15 |
2.50 |
Length mm |
350 |
350 |
350 |
350 |
Wt. per Carton Kg. |
2.0 |
2.0 |
2.0 |
2.0 |
Wt. per Box, Kg. |
10 |
10 |
10 |
10 |
